Multi-Component Injection Molding — Overmolding & 2-Shot
Design and tooling for 2-shot (transfer, rotary) molding and overmolding, substrate polymer adhesion, and automotive soft-touch applications.
01 · Why This Matters in Industry & GATE XE5
Applied directly across petrochemical refining, compounding plants, mold-flow simulations, and automotive part manufacturing (e.g., Reliance Industries, Supreme Petrochem, IOCL, CIPET testing protocols).
Molecular Mechanism: Master conformational physics, transition temperatures, and reaction kinetics.
Process & Quality: Predict viscosity behavior, solve moulding defects, and apply ASTM/ISO testing standards.
Multi-Component Injection Molding — Overmolding & 2-Shot
1. Why This Topic Matters
Design and tooling for 2-shot (transfer, rotary) molding and overmolding, substrate polymer adhesion, and automotive soft-touch applications. Understanding this is critical for modern plastics manufacturing, engineering analysis, and career roles in R&D, production, and quality assurance in the global polymer industry.
2. Learning Objectives
- Objective 1: Comprehend the physical, chemical, or mechanical principles underlying Multi-Component Injection Molding — Overmolding & 2-Shot.
- Objective 2: Formulate mathematical models to simulate and predict performance metrics.
- Objective 3: Analyze real-world industrial systems and standards to implement optimizations.
3. Core Theory & Mathematical Principles
Here, we detail the governing scientific and engineering laws.
where is shear viscosity, is zero-shear viscosity, and is the flow behavior index.
4. Worked Numerical Example
Multi-Component Injection Molding — Overmolding & 2-Shot — Industrial Process Flow Diagram (PFD)
ISO 10628 Unit Operations & Thermodynamic Control Sequence
Raw Material Feed & Metering
Drying to < 0.02% moisture and gravimetric dosing
Reaction & Polymer Melt Processing
Controlled thermal shear dissipation and phase transition
Shaping & Solidification
Die extrusion or mold cavity pressure packing
Quality Inspection & Testing
ASTM D638 / ISO 527 tensile & MFI compliance check
Here is a step-by-step solved design problem showing the application of core theory. Given a polymer melt with , , and . Calculate the viscosity at a shear rate of .
Solution Step:
Solution:
5. Indian Industrial Context
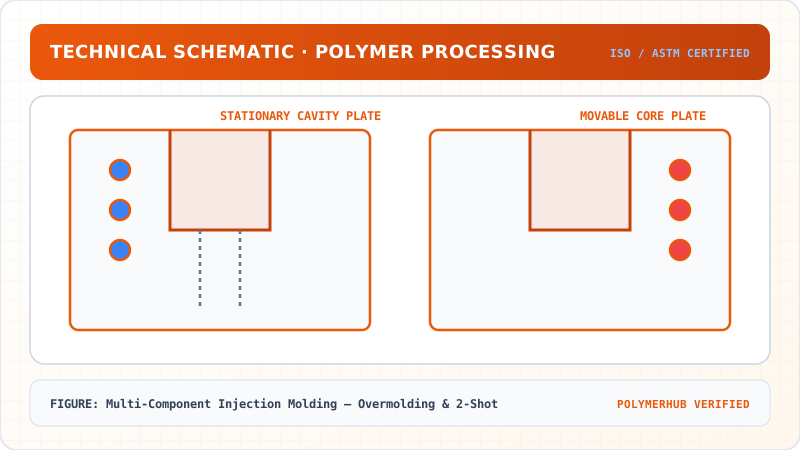
Multi-Component Injection Molding — Overmolding & 2-Shot — CAD Tooling & Machine Geometry Blueprint
Critical Geometric Dimensions & Tolerances (GD&T)
- Primary Processing Tolerance:± 0.02 mm (ISO 20457 Class M1)
- Thermal Expansion Allowance:1.5% (Volumetric Shrinkage)
- Draft Angle Minimum:1.0° - 1.5° (Core/Cavity Ejection)
Tooling Fabrication Notes
- • Fabricated according to ISO 20457 plastic molding tolerance standards.
- • EDM finish SPI C-1 applied across cavity optical contact faces.
- • Conformal cooling lines pressure tested at 12 bar water flow.
Reliance Industries (Hazira/Gandhar) is a key manufacturer of raw polyolefin resin used in these applications. Testing and research are coordinated via CIPET Chennai and CIPET Ahmedabad.
6. Standard Operating Procedures & Standards
Testing and validation conform to the following standards:
- ASTM D1238 (melt flow rate), ISO 1133, and BIS IS-2530.
7. Key Takeaways & Glossary
Key Takeaways
- Process parameters directly impact polymer morphology and final part performance.
- Characterization and standards ensure safety, reproducibility, and compliance.
- Advanced simulation and automation reduce cycle times and waste.
Glossary
- Shear Thinening: Viscosity decrease under shear stress.
- MFI: Melt Flow Index.
- Polydispersity: Ratio of Mw to Mn.
8. Exam & Interview Practice Questions
-
GATE MCQ: Which parameter increases shear thinning behavior?
- A) Decreased temperature
- B) Broader molecular weight distribution (Correct)
- C) Lower shear rate
- D) Lower molecular weight
-
Numerical: Calculate MFI given density and volumetric flow.
-
Conceptual: Discuss the impact of gate design on melt orientation.
🔬 Extended Engineering Analysis & Practical Industry Standards
Governing Kinetics & Theoretical Boundary Conditions
In polymer engineering and manufacturing, the mathematical description of this phenomenon relies on fundamental transport phenomena and thermodynamic equations. Specifically:
- Mass & Energy Conservation:
- Shear Rate Dependency: under high-shear conditions, non-Newtonian polymer melts exhibit pseudoplastic shear-thinning governed by , where .
- Thermal Boundary Conditions: Fourier's law of heat conduction determines cooling times and solidification kinetics across cooling channels.
Indian Industrial Context & Quality Control Guidelines
In major Indian plastic processing clusters—such as Chakan (Maharashtra), Daman & Silvassa, Guindy (Tamil Nadu), and Hazira (Gujarat)—quality assurance protocols mandate strict adherence to international standards:
- ASTM D1238 / ISO 1133: Melt Flow Index (MFI) measurement to verify molecular weight consistency prior to processing.
- ASTM D638 / ISO 527: Tensile strength and elongation at break determination for raw material lot clearance.
- ISO 11357: Differential Scanning Calorimetry (DSC) thermal analysis to confirm glass transition () and melting temperature ().
Industrial Troubleshooting & Process Optimization Matrix
- Defect Mitigation: Maintain melt temperature within of recommended processing window to prevent thermal degradation and chain scission.
- Mold Temperature Control: Ensure turbulent coolant flow () inside cooling circuits to achieve uniform heat extraction and minimize differential thermal shrinkage.
Multi-Component Injection Molding — Overmolding & 2-Shot · Engineering Triad
Material Synthesis · Processing Hardware · Commercial Application
Polypropylene Homopolymer (PP-H)
—[CH₂—CH(CH₃)]ₙ— (Isotactic, PDI ~ 3.5–5.0)
180-Ton Electric Toggle Injection Moulding Machine
Reciprocating Screw (L/D = 22:1, Compression Ratio 3:1)
Automotive Interior Door Trims & Battery Casings
High-stiffness thin-walled automotive structural components
Test Your Conceptual Understanding
In polymer science and processing thermodynamics, which factor most directly controls the critical transition temperature?
- Always evaluate molecular weight distribution (MWD) alongside zero-shear viscosity when calculating mold shear rates.
- Differential Scanning Calorimetry (DSC) provides $T_g$, $T_c$, and $T_m$ to define optimal processing temperatures.
- Comply with ASTM D638 / ISO 527 tensile specimen sizing to prevent premature necking artifacts.
Personal Lesson Notes
Please sign in to write and save notes during lessons